About Us
Contrary to popular belief, Lorem Ipsum is not simply random text. It has roots in a piece of classical Latin literature from 45 BC, making it over 2000 years old.
Get a free quote
Zero Liquid Discharge (ZLD)
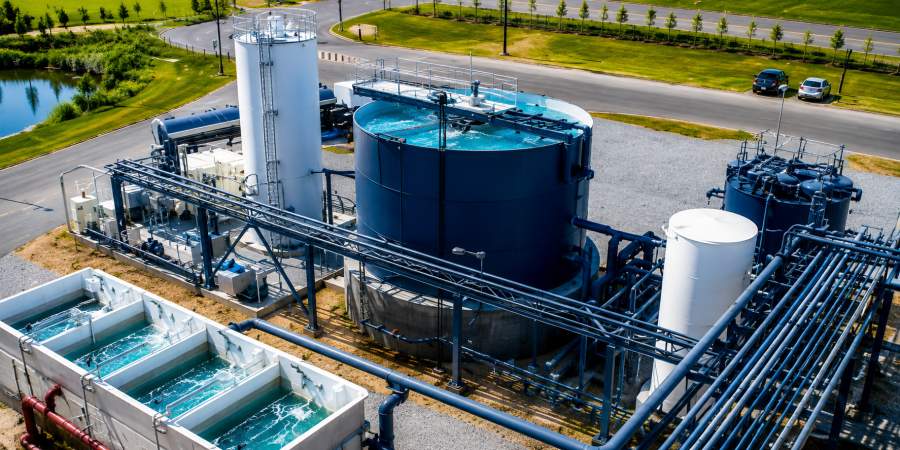
Zero Liquid Discharge (ZLD) Systems
We specialize in the Design, Fabrication, Supply, Erection, and Commissioning of advanced Zero Liquid Discharge (ZLD) Plants for complete industrial wastewater treatment. Our ZLD systems ensure 100% water recovery, eliminating liquid waste discharge into the environment while meeting strict Pollution Control Board (PCB) mandates and environmental sustainability guidelines.
With over 13 years of process engineering expertise, we manufacture energy-efficient and custom-engineered ZLD systems tailored for high-salinity and complex industrial effluents. Available as both civil-constructed installations and Compact Skid-Mounted / Modular ZLD Units, our solutions minimize site footprints, reduce civil engineering costs, and drastically lower operating expenses (OPEX).
Depending on effluent characteristics and recovery targets, we integrate state-of-the-art technologies including High-Recovery RO, Mechanical Vapor Recompression (MVR), Multiple Effect Evaporators (MEE), and Crystallizers.
Principle of ZLD Treatment
Zero Liquid Discharge is a comprehensive engineering process designed to purify and recycle all industrial wastewater. By combining advanced membrane separation with thermal evaporation and crystallization, ZLD processes separate clean, distilled water from dissolved solids and salts, leaving only dry, solid waste for safe disposal or byproduct recovery.
Treatment Steps
-
Pre-Treatment & Chemical Clarification
-
High-Recovery Membrane Pre-Concentration (RO/NF)
-
Thermal Concentration (MEE / MVR Evaporation)
-
Crystallization of Concentrated Brine
-
Solids Dewatering & Salt Recovery (Centrifuge/Filter Press)
-
Distillate Recycling to Plant Utility Systems
Thermal Evaporation & Concentration
The core of our ZLD system leverages energy-efficient thermal technology. Pre-concentrated reject water enters our Multiple Effect Evaporators (MEE) or MVR systems, where heat energy is reused across multiple stages to vaporize water efficiently, producing high-purity condensate suitable for boiler feed or process reuse.
Designed with corrosion-resistant alloys (Titanium, Duplex Stainless Steel, Hastelloy), our evaporators handle severe scaling conditions, high total dissolved solids (TDS), and harsh chemical loads without operational interruption.
Key Technical Advantages
- 100% Water Recycling – Reclaims up to 95–99% of wastewater as pure water, significantly cutting fresh water consumption costs.
- Guaranteed Regulatory Compliance – Completely avoids legal penalties and risks of plant shutdown by eliminating liquid discharge.
- Optimized Thermal Efficiency – Low energy MVR and MEE integration dramatically lowers steam and power costs.
- Anti-Scaling & Fouling Engineering – Specialized heat exchanger designs prevent scaling during high TDS concentration.
- Corrosion-Resistant Fabrication – Meticulously selected metallurgy guarantees long equipment operational life under harsh environments.
- Resource & Salt Recovery – Allows recovery of valuable chemical byproducts (e.g., Sodium Sulfate, Sodium Chloride) for reuse.
- Automated PLC/SCADA Control – Fully automated operation minimizes manual intervention and optimizes operational stability.
Key Benefits for Industries
- Complete Environmental Security – Zero risk of ground or surface water contamination.
- Water Independence – Protects production schedules against municipal water scarcity and tariff hikes.
- Custom Scalability – Engineered for capacities ranging from 5 m³/day up to multi-megaliter industrial plants.
- Enhanced ESG & Sustainability Score – Positions your business as an environmentally responsible market leader.
- Turnkey Project Execution – Single-source accountability from water testing to final commissioning.