About Us
Contrary to popular belief, Lorem Ipsum is not simply random text. It has roots in a piece of classical Latin literature from 45 BC, making it over 2000 years old.
Get a free quote
Water Bottling Plant
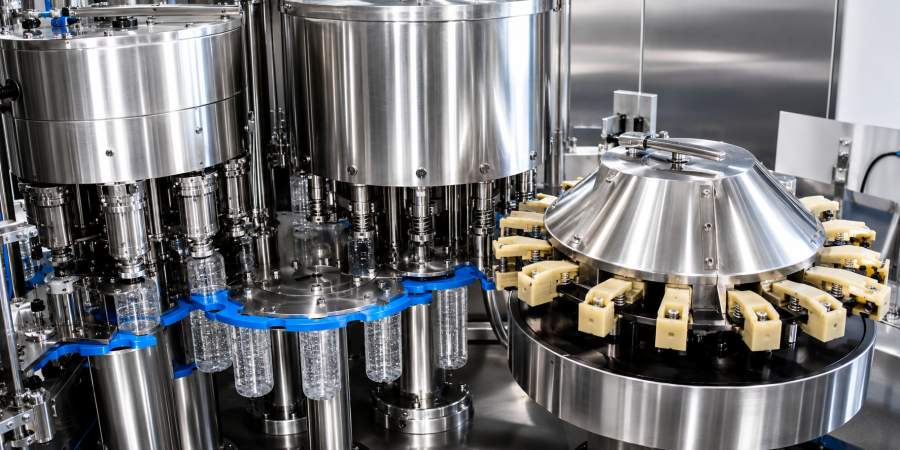
Turnkey Water Bottling Plants
We specialize in the Design, Fabrication, Supply, Erection, and Commissioning of advanced Turnkey Water Bottling Plants for commercial packaged drinking water production. Our automated bottling solutions ensure 100% hygienic processing, precision filling, and reliable packaging while meeting strict BIS (Bureau of Indian Standards), FSSAI, and international food safety guidelines.
With over 13 years of process engineering expertise, we manufacture energy-efficient and custom-engineered water bottling lines tailored for diverse container formats. Available as both high-capacity fully automatic lines and Compact Skid-Mounted / Semi-Automatic Bottling Units, our solutions minimize site footprints, optimize utility costs, and drastically lower operating expenses (OPEX).
Depending on source water quality and production capacity targets, we integrate state-of-the-art technologies including Ozonation, Reverse Osmosis (RO), Ultrafiltration (UF), Automatic Blow Molding, and High-Speed Filling Systems.
Principle of Bottling Plant Operations
A Turnkey Water Bottling Plant operates as a seamless multi-stage engineering process designed to purify raw water and package it safely for consumers. By combining advanced multi-stage water purification with fully automated blowing, rinsing, filling, capping, and labeling systems, our plants deliver premium quality drinking water with minimal human contact and maximum shelf-life.
Process Steps
-
Raw Water Clarification & Pre-Filtration
-
Advanced RO & UV / Ozonation Sterilization
-
Automatic PET Bottle Stretch Blow Molding
-
Automatic Rinsing, Filling & Capping (RFC Monoblock)
-
Labeling, Batch Coding & Shrink Wrapping
-
Final Product Quality Testing & Palletizing
Automated Purification & Packaging Technology
The core of our Water Bottling Plant combines high-precision water treatment with high-speed packaging machinery. Treated water passes through multi-grade filtration, active carbon absorption, RO membranes, and ozone mineralization, ensuring perfect taste, crystal-clear purity, and strict microbiological compliance.
Constructed using food-grade Stainless Steel (SS304/SS316L), our bottling lines prevent cross-contamination, resist chemical corrosion, and support CIP (Clean-In-Place) systems for continuous, hygienic production without unnecessary downtime.
Key Technical Advantages
- High-Purity Purification – Advanced RO, UV, and Ozonation yield premium-grade drinking water meeting BIS and WHO standards.
- Guaranteed Regulatory Compliance – Designed to pass mandatory food safety, FSSAI, and ISI license inspections effortlessly.
- Optimized Energy & Bottle Yield – Low power consumption systems paired with high-efficiency blowers reduce operational costs.
- Hygienic Monoblock Architecture – Integrated Rinsing-Filling-Capping eliminates airborne contamination risk during filling.
- Food-Grade SS Fabrication – Heavy-duty Stainless Steel construction guarantees long equipment service life and sanitary processing.
- Flexible Packaging Formats – Easily adapts to fill 200ml, 500ml, 1L, 2L, and 20L jar containers on the same line.
- Automated PLC/HMI Touchscreen Control – Fully integrated PLC control enables real-time monitoring of filling accuracy and line speed.
Key Benefits for Business Owners
- Zero-Contamination Guarantee – Enclosed, touch-free filling zones prevent bacterial contamination and preserve shelf stability.
- Market-Ready Production – High-speed output options let you scale operations fast to meet local demand.
- Custom Line Scalability – Configurable capacities ranging from 2,000 Bottles/Hour (BPH) up to 24,000 BPH automated plants.
- High Return on Investment (ROI) – Reduced wastage, precise fill-volume accuracy, and low maintenance maximize profit margins.
- Turnkey Project Execution – Complete single-source solution from raw water analysis and layout design to machine installation and commissioning.