About Us
Contrary to popular belief, Lorem Ipsum is not simply random text. It has roots in a piece of classical Latin literature from 45 BC, making it over 2000 years old.
Get a free quote
Dialysis RO Plant
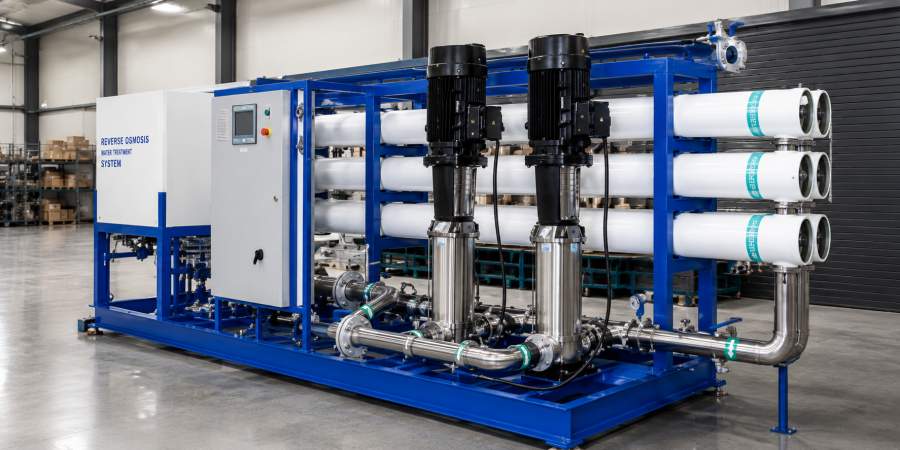
Dialysis Reverse Osmosis (RO) Plants
We specialize in the Design, Fabrication, Supply, Erection, and Commissioning of high-purity Dialysis Reverse Osmosis (RO) Plants for hospitals, hemodialysis centers, and clinical laboratories. Our medical-grade RO systems deliver ultra-pure, pyrogen-free water, ensuring strict compliance with international medical standards such as ISO 23500, AAMI, and Pharmacopeia guidelines.
With over 13 years of process engineering expertise, we engineer redundant, double-pass RO and continuous EDI (Electrodeionization) systems tailored for critical patient safety. Available as both custom plant installations and Compact Skid-Mounted / Modular Dialysis RO Units, our systems offer continuous sanitization, quiet operation, and minimal site footprints.
Depending on feed water composition and dialyzer demand, we integrate state-of-the-art technologies including Dual-Pass RO, Micro/Ultrafiltration, Hot Water Sanitization (HWS), UV Disinfection, and Endotoxin Retention Filters.
Principle of Medical-Grade Water Purification
Dialysis water treatment is a high-precision multi-stage purification process engineered to completely remove dissolved inorganic salts, organic contaminants, bacteria, and microbial endotoxins (pyrogens). By utilizing dead-leg-free circulation loops and continuous microbiological control, our systems ensure ultra-pure water is reliably delivered directly to hemodialysis machines without risk of secondary contamination.
Treatment Steps
-
Multi-Media Filtration & Softening Pre-Treatment
-
Dual-Stage Activated Carbon Filtration (Dechlorination)
-
High-Rejection Primary Reverse Osmosis Pass
-
Polishing Secondary RO Pass / Continuous EDI
-
Thermal (Hot Water) or Chemical Sanitization
-
Ultrafiltration & Endotoxin Retention Loop
Microbiological Control & Thermal Sanitization
The core of our Dialysis RO system relies on stringent bio-burden management. To prevent biofilm growth, our systems incorporate automated Hot Water Sanitization (HWS) sequences at >85°C or integrated ozone-assisted disinfection loops that sanitize the entire membrane stack and distribution ring main without harmful chemicals.
Constructed with orbital-welded SS316L sanitary piping and smooth, electro-polished surfaces, our plants eliminate dead legs and stagnant zones to ensure uncompromised microbiological safety for dialysis patients.
Key Technical Advantages
- Ultra-Pure Water Delivery – Consistently achieves conductivity <1 µS/cm and endotoxin levels <0.03 EU/mL.
- ISO 23500 & AAMI Compliant – Guaranteed compliance with global medical and hemodialysis purity standards.
- Redundant Dual-Pass Architecture – Ensures uninterrupted purified water supply even during single-component maintenance.
- Automated Hot Water Sanitization – Thermal self-sanitization eliminates chemical handling and downtime.
- SS316L Sanitary Construction – High-grade stainless steel piping prevents bacterial adhesion and corrosion.
- Continuous Microbiological Monitoring – Integrated TOC, conductivity, and temperature sensors for real-time safety tracking.
- Smart PLC/HMI Controls – Intuitive automated interface with data-logging and remote alarm alerts.
Key Benefits for Healthcare Centers
- Maximized Patient Safety – Zero-tolerance engineering against pyrogens, heavy metals, and bacteria.
- Uninterrupted Clinical Up-time – Designed with redundant standby pumps and membranes for 24/7 reliability.
- Custom Capacity Options – Scalable systems designed to support from 5 up to 100+ dialysis beds simultaneously.
- Audit-Ready Documentation – Complete IQ/OQ validation protocols and compliance records provided.
- Turnkey Clinical Execution – Complete support from water analysis and system design to validation and operator training.